Our Premium Soup Bowl Solutions



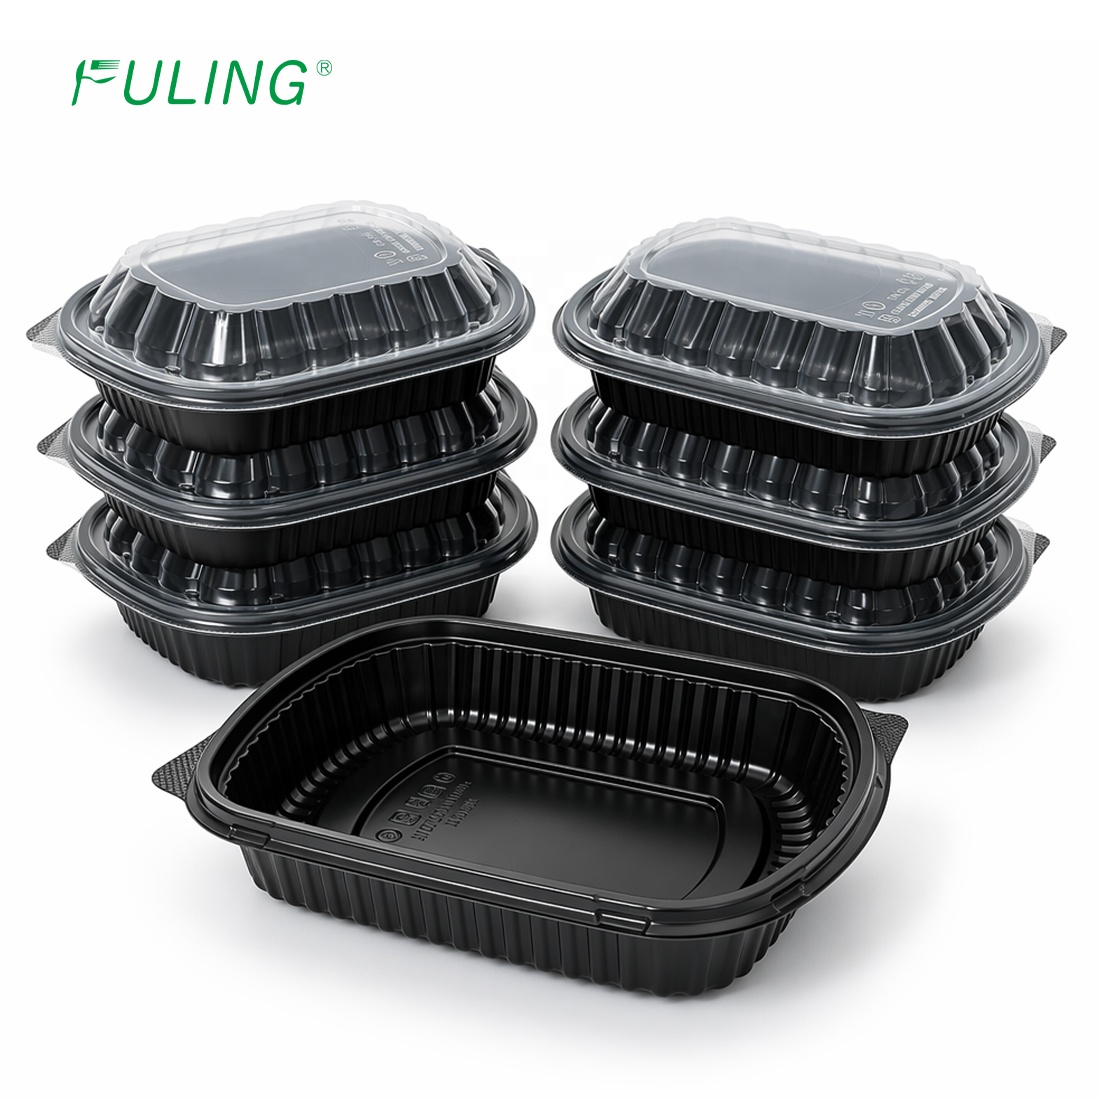
Strategic Partnership for the Victoria Market
As a leading Chinese manufacturer, we specialize in high-durability plastic soup bowls tailored for the unique requirements of the Victoria foodservice landscape. Victoria’s thriving cafe and takeaway culture demands packaging that is not only leak-proof but also microwave-safe and aesthetically professional. Our factory integrates advanced injection molding technology, ensuring that our soup bowls maintain structural integrity under high heat—a critical requirement for local soup delivery services.
Industry Trends and Localized Application
The Victoria market is rapidly shifting towards sustainable yet high-performance packaging. Our "Information Gain" approach focuses on providing the market with hybrid PP (Polypropylene) solutions that offer superior clarity and thermal resistance. From bustling urban bistros to remote catering events, our products are engineered to reduce food waste and enhance the end-customer's dining experience.
Why Choose Our Manufacturing Facilities?
Our commitment to E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) is evident in our standardized production lifecycle. We maintain rigorous quality control measures, ensuring all items comply with international food-contact safety standards (FDA/LFGB). Unlike generic suppliers, we provide comprehensive technical documentation, including raw material certificates and detailed migration test reports, facilitating smoother customs clearance for Australian distributors.
Frequently Asked Questions
Q: Are your soup bowls compatible with automatic filling machines?
A: Yes, our injection-molded bowls feature uniform rim dimensions designed for high-speed automated filling lines used by industrial kitchens.
Q: How do you ensure consistency for Victoria-based retailers?
A: We utilize multi-cavity precision molds and laser-measured quality checkpoints to ensure that the 50,000th unit is identical to the first, minimizing shrinkage and deformation during long-distance transit.
Q: Can I request custom branding?
A: Absolutely. We offer IML (In-Mold Labeling) and high-quality pad printing options to help your brand stand out in the competitive local market.
Detailed Manufacturing Expertise
Our facility operates 24/7 with a focus on high-efficiency output. By optimizing our supply chain, we offer Victoria buyers a competitive advantage through reduced lead times and consolidated LCL (Less than Container Load) shipping options. Whether you are a small distributor or a large catering chain, our flexible MOQ policy allows you to scale your inventory according to seasonal demand fluctuations common in the Victoria hospitality sector.
Our technical team performs weekly stress tests—simulating 95°C hot-fill conditions and drop tests at -18°C—to guarantee our bowls perform perfectly, whether for hot soup delivery or frozen meal prep applications. This level of technical validation is why we remain the preferred partner for businesses that cannot afford packaging failure.