


Strategic Partnership for Banja Luka Foodservice Providers
In the evolving hospitality market of Banja Luka, reliable disposable food packaging is the backbone of operational efficiency. As a leading manufacturer and exporter, we specialize in providing high-performance hot drink cups that balance thermal retention with environmental compliance. Our deep understanding of E-E-A-T (Experience, Expertise, Authoritativeness, Trustworthiness) ensures that every cup we supply meets rigorous food-contact safety standards, including FDA 21 CFR and EU 10/2011 protocols.
The Information Gain Advantage
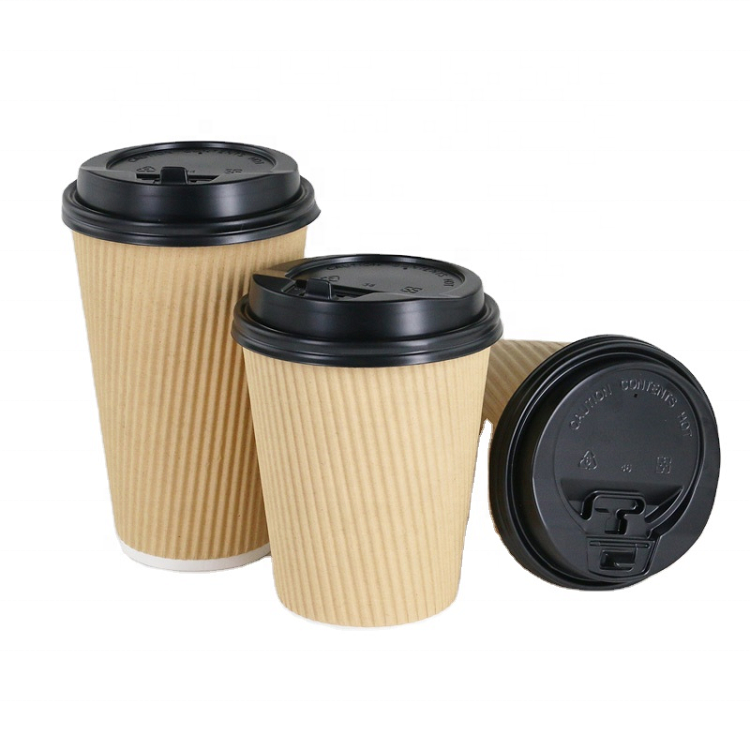
Unlike generic wholesalers, we provide a "technical edge" for your business. We help importers analyze the trade-off between insulation properties and manufacturing costs. By utilizing advanced ripple-wall technology, our hot drink cups prevent heat transfer while maintaining a structural integrity that withstands the humidity fluctuations common in regional transport. Our Information Gain approach involves providing you with material migration data, precise gram-weight optimization reports, and lid-fit tolerance analysis before you commit to large-scale production.
Local Application Scenarios & Trends
Banja Luka’s coffee culture is undergoing a shift toward premium, on-the-go experiences. This requires packaging that signals quality. Our products serve three primary local applications:
- Boutique Cafés: Custom-branded double-wall cups that keep beverages hot for longer periods.
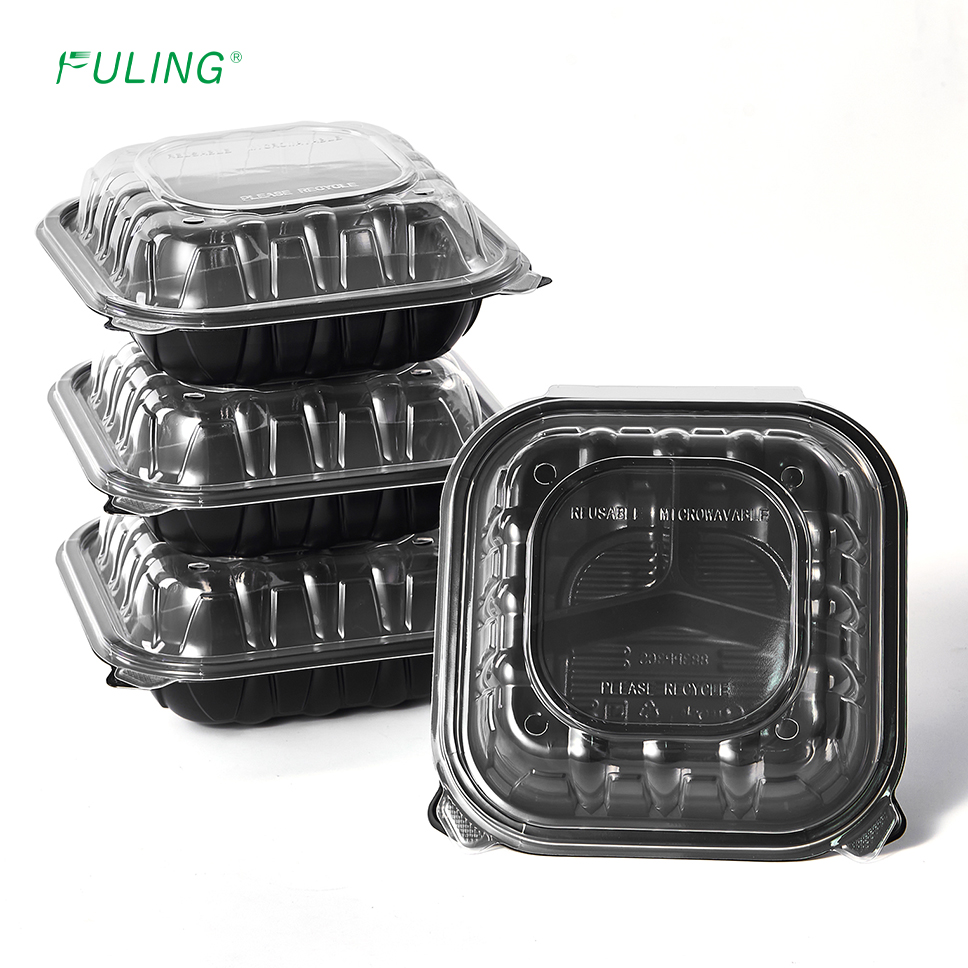
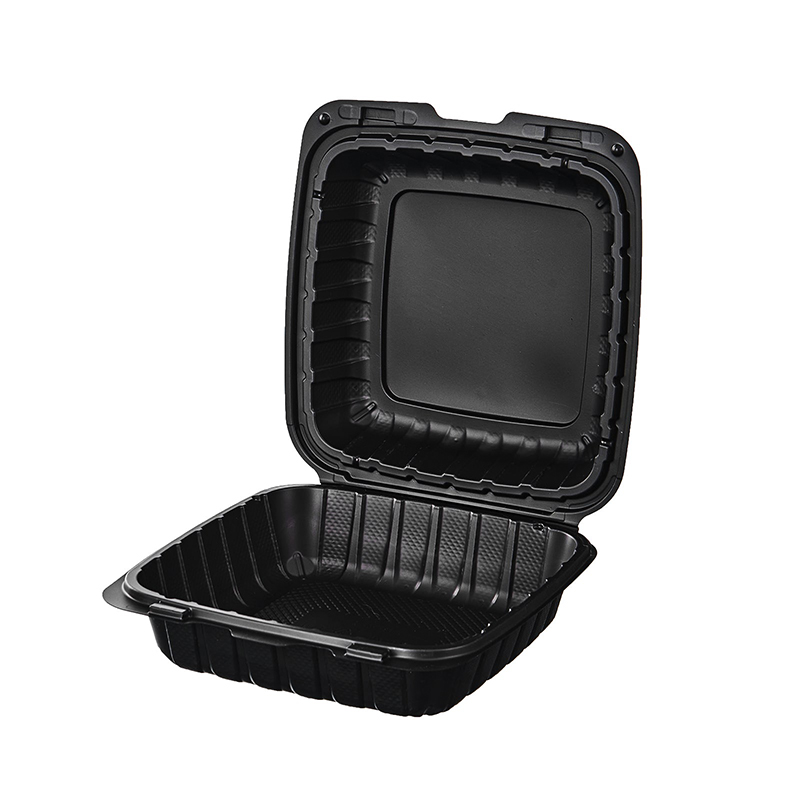
- Food Delivery Ecosystems: Leak-resistant containers that survive multi-stop logistics without compromising food temperature.
- Catering Services: Sustainable, rigid tableware options that replace fragile or harmful plastic alternatives.
Frequently Asked Questions
What makes your hot drink cups superior for export?
We use high-density, food-grade paperboard coupled with aqueous-based coatings that reduce plastic usage while enhancing printability. Our "no-crush" packaging technology ensures that cups arrive in Banja Luka in perfect round shape, preventing common leakage issues.
Can we request custom branding for small batches?
We bridge the gap between small-batch needs and industrial scale. Our flexible OEM/ODM workflow allows for strategic customization even for growing chains.
How do you ensure food safety compliance?
We provide full documentation for every shipment, including independent third-party test reports for heavy metals, OML (Overall Migration Limit), and PFAS-free certification.
Why Choose Our Manufacturing Direct Services?
We are not just a supplier; we are your production arm in China. With over 20 years of expertise in injection molding and paper forming, we provide a seamless bridge to high-quality manufacturing. Our enterprise advantage lies in our "Full-Chain QC," where we monitor every stage from the resin pellet to the final palletization, ensuring consistent quality that scales with your business.